
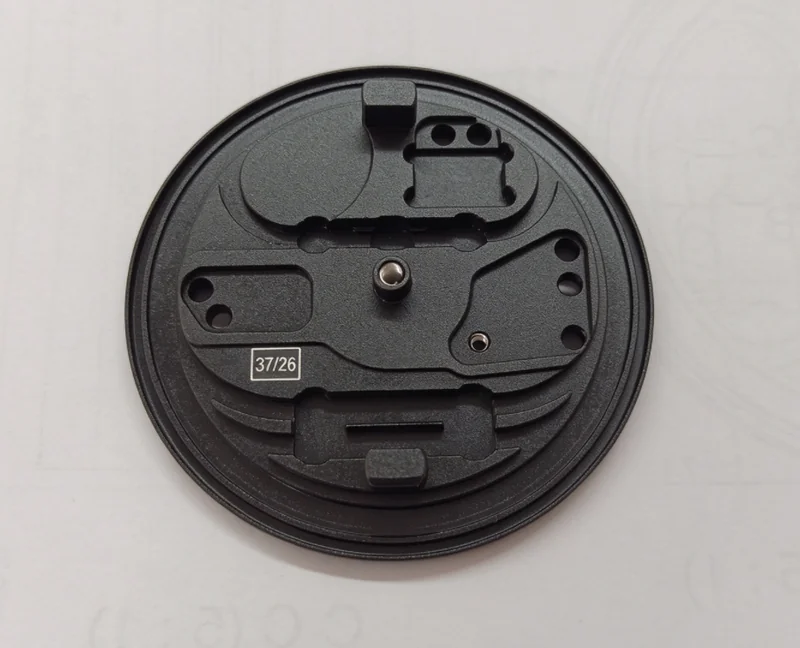
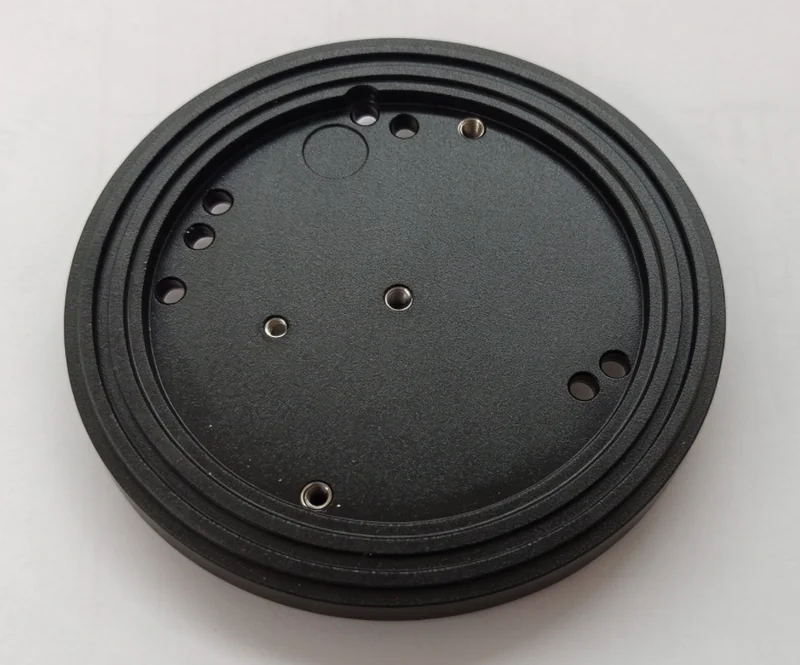
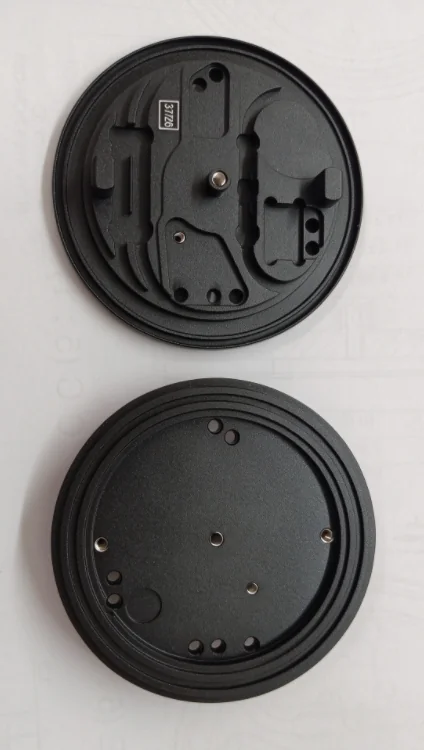
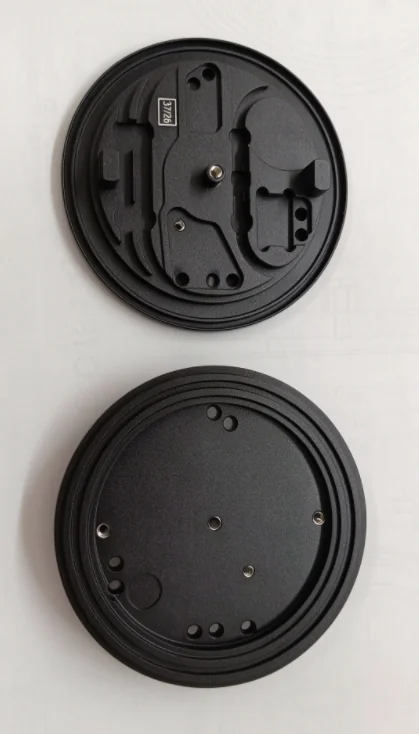
An AL6061 circular base plate finished with fine bead blasting and bright black anodizing at a film thickness of 8–10 µm, with the thread holes de-oxidised. The plate carries built-in M2 thread inserts (Heli-Coil), so insert seating and surface appearance have to be controlled together.
| Part | Circular base plate |
|---|---|
| Material | AL6061 |
| Surface | Fine bead blast + bright black anodizing, film 8–10 µm, matched to sample |
| Thread inserts | M2 Heli-Coil, pre-installed |
| Internal fillets | ≤0.2 mm |
| Features | Multiple internal grooves and hole positions, several with local tight tolerances |
| Marking | Laser marking of manufacturing week / year at a specified position |
The Challenge
M2 Heli-Coil insert installation
An M2 thread insert must be pre-installed. The end face of the insert must not stand above the product surface — it has to sit sunk into the workpiece. Material certificates for the insert must be supplied before assembly, and the assembly precision itself is difficult to control.
Selective oxide removal on the thread holes
The plate is anodized black overall, but the threaded holes need the oxide layer removed so the inserts can be assembled. Masking and post-processing must be controlled carefully to avoid scratching the surrounding black anodized surface.
Sharp edges and fillet control
No chamfers may be added on our own initiative. The internal fillet is ≤0.2 mm, and sharp edges may only be lightly sanded to remove burrs. Holding the fillet size stable is difficult.
Bead-blasted appearance and anodizing
Fine bead blasting must be uniform, and the bright black anodizing is matched to the sample at 8–10 µm. The risk of the anodized colour fading has to be investigated, and the racking (hanging) points controlled.
Multi-cavity, multi-hole tolerances and flatness
The plate contains multiple internal grooves and hole positions, several with tight local tolerances. Machining a disc of this type easily produces flatness deformation, which affects assembly.
Laser marking
Manufacturing week and year are marked at the specified position, without damaging the surrounding anodized appearance.
What the Project Requires
- •M2 Heli-Coil inserts pre-installed and sunk below the surface, with material certificates provided before assembly.
- •Masking and post-processing controlled so the oxide is removed only from the thread holes, leaving the surrounding black anodized surface unscratched.
- •No added chamfers — internal fillet ≤0.2 mm, sharp edges sanded only to remove burrs.
- •Uniform bead blast and bright black anodizing matched to the sample at 8–10 µm, with racking points controlled against fading.
- •Flatness controlled during machining of the multi-cavity disc so assembly is not affected.
- •Laser marking of manufacturing week / year without damaging the anodized appearance.
Need thread inserts installed and anodized correctly? Send the drawing and insert specification — our team reviews precision machining, Heli-Coil installation and selective anodizing controls.